Torque Testing Trigger Sprayers and Pump Dispensers: A Practical Procedure Guide
Step-by-step torque test procedure for trigger sprayers and pump dispensers. Covers fixturing, specs by industry (cleaning, cosmetics, pharma), ASTM D3198, and failure modes.
A trigger sprayer that passes every spray-pattern and output test can still leak on the shelf if the torque that locks it to the bottle was never tested as a standalone parameter. A torque test for trigger sprayers and pump dispensers measures the rotational force applied to thread these closures onto bottle neck finishes, and the force required to remove them. Published benchmarks place pump dispenser application torque at 0.8–0.85 N.m, though the correct value shifts with neck finish size, closure material, and the product inside the bottle. This guide covers equipment setup, torque specifications across three industries, a step-by-step testing procedure, and the failure modes that out-of-spec torque creates in sprayers and pumps.
Why Torque Is the QC Step That Trigger Sprayers and Pump Dispensers Keep Losing
Torque testing for threaded closures is standard practice on bottling lines. For screw caps. Trigger sprayers and pump dispensers often skip the standalone torque check because they undergo other functional tests (spray output, leak checks, actuation force) that seem to cover the same ground. They do not. Incorrect production-line torque settings cause two distinct failures: compromised pump performance and leakage at the neck seal.
Both trigger sprayers and pump dispensers thread onto standard bottle neck finishes. The two most common sizes are 28-400 and 24-410, the same finishes used for standard screw caps. But pump mechanisms add internal spring resistance that changes how torque translates to seal compression, and trigger sprayers have longer lever arms that alter the user's perception of tightness during manual assembly checks.
| Closure Type | Common Neck Finishes | Why Torque Behaves Differently Than Screw Caps |
|---|---|---|
| Trigger sprayer | 28-400, 24-410 | Extended lever arm above closure ring shifts perceived tightness; siphon tube alignment depends on thread engagement angle |
| Pump dispenser | 24-410, 28-400 | Internal spring mechanism resists rotation during application, inflating the torque reading if not accounted for |
So what torque value should you actually target, and does it change depending on what is inside the bottle?
Equipment Setup — Fixturing Trigger Sprayers and Pump Dispensers for Accurate Readings
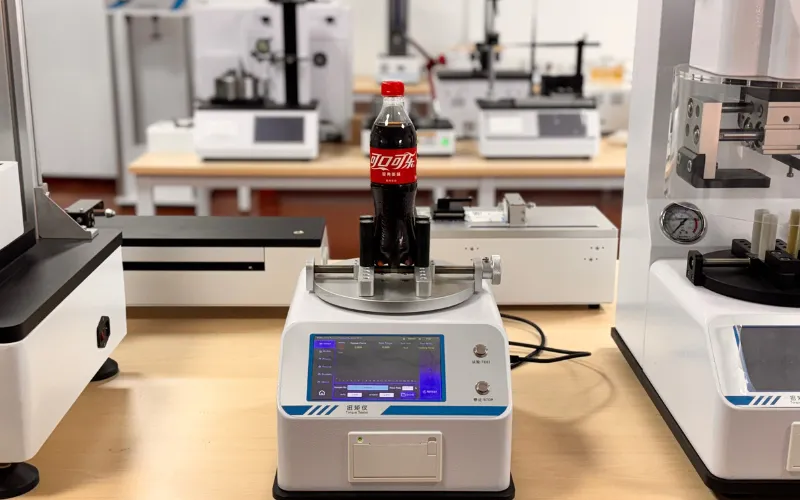
Fixture setup starts with the instrument itself. In the well-documented Pfeiffer/Aptar Pharma case, a Tornado-series manual torque tester measured both clockwise and counter-clockwise movement. Four gripping pegs on the tester base hold the bottle still, preventing rotation during measurement.
Where trigger sprayers and pump dispensers differ from screw caps is geometry. A screw cap sits flush with the bottle neck. A pump dispenser extends several centimeters above the closure ring, and a trigger sprayer reaches further still with its nozzle and lever assembly. Apply torque at the closure collar only, the threaded ring that contacts the bottle neck, not at the pump head or trigger body. Gripping the wrong surface adds mechanical resistance from the pump or trigger mechanism to the reading.
ASTM D3198 is the governing standard for measuring application and removal torque on threaded closures. It applies to any threaded closure type, including trigger sprayers and pump dispensers on standard neck finishes.
| Setup Step | What to Check | Why It Matters |
|---|---|---|
| Fixture fit | Gripping pegs contact bottle body without deforming it | Bottle rotation during test invalidates the reading |
| Grip point | Torque applied at closure collar, not pump head or trigger body | Prevents contamination of reading with internal mechanism resistance |
| Zeroing | Tester reads zero before each sample | Drift between samples compounds into systematic error |
| Sample conditioning | Samples at controlled temperature and humidity | Polymer thread friction changes with temperature |
Pre-test checklist. Verify these four items before the first test run: fixture pegs match bottle diameter, tester is zeroed, samples have been conditioned to ambient temperature for a minimum of two hours, and the grip adapter contacts only the closure collar.
Torque Specs by Industry — Household Cleaning, Cosmetics, and Pharma Do Not Share a Number
Household Cleaning Products — Chemical Resistance Drives the Torque Window
For household cleaning trigger sprayers, chemical compatibility between the formula and the PP sprayer body is the factor that narrows the acceptable torque range. Aggressive solvents and concentrated surfactants swell or soften polypropylene over time, which means the torque that felt secure at filling can loosen on the shelf as the material changes dimensionally.
Run a 24–48 hour chemical soak test on sprayer components, submerging the PP body and other components (HDPE, LDPE, or PET parts) in the actual formula, before setting the final torque specification. Over-torquing is especially risky with cleaning products because stress-cracking from chemical exposure compounds with mechanical stress from excessive thread compression.
If your formula contains solvents or surfactants above typical household concentrations, run the soak test before you lock in a torque spec — not after.
| Factor | Effect on Torque Specification |
|---|---|
| Solvent concentration in formula | Higher concentration narrows acceptable torque range (risk of stress cracking at upper end) |
| PP sprayer body | Dimensional swelling after chemical exposure can reduce effective seal torque over shelf life |
| Soak test (24–48 hours) | Determines whether initial torque holds after chemical exposure; must be run before setting production spec |
Cosmetics and Personal Care — Pump Dispensers and the 0.8–0.85 N.m Benchmark
Cosmetics pump dispensers have a well-documented torque range: 0.8–0.85 N.m, established in the Pfeiffer (now Aptar Pharma) testing program for pharmaceutical and cosmetics pump products. This number assumes a specific neck finish and pump design. Cosmetics packaging often uses 24-410 neck finishes and decorative over-caps that change the torque interaction because the over-cap applies additional downward force on the pump collar, supplementing the thread engagement.
Dip tube fit testing should happen alongside torque verification. The dip tube is measured from the gasket bottom to the end notch, and flexible dip tubes typically add approximately one inch to the bottle height requirement. Off-axis torque application, where the pump is threaded slightly crooked, is a common cosmetics packaging defect that misaligns the dip tube and causes inconsistent dispensing.
Pharmaceutical and Healthcare — Documentation and Validation Sit on Top of the Torque Number
In pharmaceutical applications, the torque value itself is only the starting point. The validation protocol, sampling plan documentation, and retention testing over stability intervals are what regulatory audits actually examine. The Pfeiffer/Aptar pharma pump testing program established the 0.8–0.85 N.m benchmark specifically for pharmaceutical dosing pumps.
Pharma pump dispensers often dispense metered doses, making torque consistency critical to dosing accuracy. A loose pump shifts the actuation stroke because the pump housing moves relative to the bottle, changing the effective displacement volume. Incorrect production-line torque settings in pharma do not just cause leakage; they can alter dose delivery, turning a packaging issue into a regulatory failure.
| Industry | Primary Torque Concern | Testing Implication |
|---|---|---|
| Household cleaning | Chemical compatibility erodes torque retention over shelf life | Soak test (24–48 hrs) before setting spec; re-test after aging |
| Cosmetics / personal care | Decorative over-caps and dip tube alignment interact with torque | Test with and without over-cap; verify dip tube position after torque application |
| Pharmaceutical | Regulatory documentation and dose accuracy depend on torque consistency | Validated test protocol with full traceability; stability-interval re-testing |
Step-by-Step — Running the Torque Test from First Sample to Pass/Fail Decision
Follow this eight-step procedure for each sample:
1. Condition samples. Stabilize filled assemblies at controlled temperature and humidity. Pump dispensers filled with product behave differently than empty assemblies because the liquid column inside the dip tube adds mass that affects how the closure seats during capping.
2. Secure the bottle in the fixture. Place the bottle between the four gripping pegs. Confirm the bottle cannot rotate by applying light lateral pressure. If the bottle shifts, the torque reading will include friction between the bottle and the fixture rather than between the closure threads and the neck finish.
3. Measure application torque (clockwise). Rotate the closure in the tightening direction and record the peak torque value. For pump dispensers, a reference benchmark is 0.8–0.85 N.m; trigger sprayer specifications depend on neck finish size and industry.
Why test seal integrity between the two torque measurements? Because a pump dispenser can hit the correct application torque and still leak. The seal check isolates whether torque is actually creating a functional closure.
4. Verify seal. Invert the bottle or apply a pressure/vacuum test to confirm the closure is sealing at the measured application torque.
5. Measure removal torque (counter-clockwise). Rotate the closure in the loosening direction and record the peak removal torque value. The relationship between application and removal torque reveals whether thread engagement is functioning correctly. For a deeper look at what the ratio tells you, see application torque versus removal torque.
6. Calculate the ratio. Compare application torque to removal torque against the specification for your closure and neck finish combination.
7. Log results per ASTM D3198 reporting requirements. Record peak values, sample identification, date, operator, and instrument calibration status.
8. Determine pass/fail. Compare each sample's application and removal torque values against the acceptance criteria for the specific closure, neck finish, and industry requirements.
| Step | Measurement | Key Consideration |
|---|---|---|
| 3 | Application torque (CW) | Record peak value; benchmark 0.8–0.85 N.m for pump dispensers |
| 4 | Seal verification | Invert or pressure test between torque measurements |
| 5 | Removal torque (CCW) | Record peak value; compare ratio to application torque |
| 8 | Pass/fail decision | Compare against spec for closure type, neck finish, and industry |
Sample size guidance: Test a minimum of 10 units per production lot. For multi-cavity molds, test at least one unit per cavity position per lot to catch cavity-specific variation in thread dimensions.
Common Failures — What Out-of-Spec Torque Actually Does to Sprayers and Pumps
Out-of-spec torque produces different failure modes depending on direction:
Under-torque failures:
- Leakage at the neck seal because the gasket does not compress enough to form a reliable barrier
- Pump dislodgment during shipping, where vibration and impact forces overcome insufficient thread engagement
- Loss of prime when air enters the dip tube path through the incomplete seal, breaking the siphon that the pump depends on
Over-torque failures:
- Cracked pump housing. PP is brittle under high thread compression, and the closure ring can fracture the pump body
- Cross-threaded neck finish, especially common on 28-400 closures with fine thread pitch, where excess force can jump threads
- Restricted pump actuation because the spring mechanism binds when the housing is compressed beyond design tolerance
For trigger sprayers specifically, over-torque can deform the siphon tube entry angle where it passes through the closure. This changes the spray pattern geometry and degrades dispenser function in a way that only shows up during output testing, not during visual inspection.
| Torque Direction | Failure Mode | Mechanism |
|---|---|---|
| Under-torque | Leakage at neck seal | Gasket under-compressed |
| Under-torque | Loss of prime | Air ingress through incomplete seal breaks siphon |
| Over-torque | Cracked pump housing | PP fractures under excessive thread compression |
| Over-torque | Spray pattern degradation (trigger sprayers) | Siphon tube entry angle deformed by housing compression |
After any torque adjustment on the capping line, re-run the spray pattern and output test (minimum 30 trigger presses into a measuring cup) to confirm the mechanical change did not degrade dispenser function.